

Precision vs Standard Injection Moulding: Understanding Micron-Level Standards
In modern manufacturing, precision injection moulding has become a critical technology in high-end industries such as electronics, automotive, and medical devices. Compared to standard injection moulding, it ensures higher dimensional accuracy, consistent quality, and superior surface finish. Implementing comprehensive process standards across materials, mould design, processing, inspection, and equipment management is essential to achieve micron-level precision.
This article explains the key dimensions of precision injection moulding and why it outperforms conventional processes.
Raw Material Control: The Foundation of Precision
The stability of raw material properties directly determines the accuracy of molded components. A three-step screening process is recommended:
- Particle Size Analysis: Use a laser particle size analyzer to confirm uniformity, with a deviation ≤0.02 mm.
- Melt Index Analysis: Employ differential scanning calorimetry (DSC) to ensure batch-to-batch melt index fluctuation remains within ±5%.
- Moisture Testing: For hygroscopic materials (e.g., PA, PC), moisture content must be below 0.02%. If necessary, dry under vacuum at 80–120°C for 4–6 hours.
Storage must follow the FIFO principle, with ambient conditions maintained at 23±2°C and 45–60% relative humidity. Materials should be stored by grade and clearly labeled to prevent cross-contamination. Batch records—including manufacturer, production date, and shelf life—should be meticulously logged for traceability.
Mold Design: The Core of Accuracy

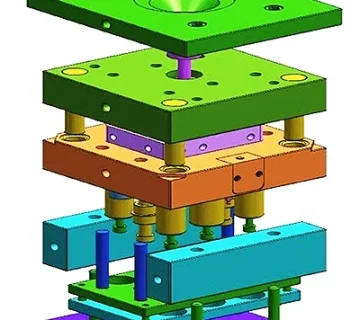
- Machining Tolerance: Mold machining precision must reach IT5 standard, with cavity and core tolerances within ±0.005 mm.
- Hot Runner Systems: Gate diameters should be one-third to one-half of the wall thickness, supported by closed-loop temperature control (variance ≤±1°C).
- Venting: Exhaust slot depth ≤0.01 mm, width 5–10 mm, to avoid burns and short shots.
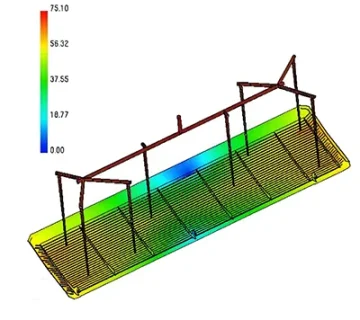
- Cooling: Water channels should be 15–25 mm from the cavity, with flow velocity 1.5–3 m/s, ensuring temperature uniformity within ±2°C.
- Guiding Mechanism: The clearance between guide posts and bushings should be ≤0.003 mm to ensure precise mold alignment.
| Aspect | Precision Injection Moulding | Standard Injection Moulding |
|---|---|---|
| Dimensional Tolerance | ±0.01 mm or better (micron-level) | ±0.05–0.1 mm |
| Surface Quality | High gloss, no defects ≥0.1 mm (microscopy checked) | Acceptable minor surface marks |
| Materials | Special engineering plastics (PA, PC, PEEK, LCP) with strict moisture & property control | Commodity plastics (PP, PE, PS, ABS) with general quality control |
| Mould Design Tolerance | IT5 standard; cavity/core precision within ±0.005 mm | IT7–IT8 standard; general machining tolerances |
| Processing Environment | Cleanroom (ISO Class 8); controlled T=22±1°C, RH=50%±5% | Normal workshop conditions |
| Applications | Medical devices, electronics, optical components, automotive safety parts | Consumer goods, household items, general industrial parts |
| Quality Inspection | CMM with 0.001 mm accuracy; CPK ≥1.33; long-term traceability | Vernier callipers or gauges; general QC checks |
| Production Cost | Higher (due to advanced moulds, cleanroom, inspection, equipment maintenance) | Lower (standard tools, less strict environment, faster cycle) |
| Output Value | High-performance, safety-critical components | Mass-market, cost-driven products |
Injection Parameter Optimization
Balancing Pressure, Speed, and Temperature
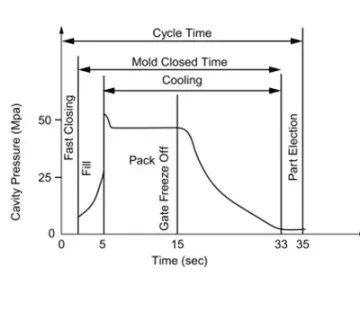
The molding process requires dynamic precision in pressure, velocity, and temperature:
- Filling Stages:
- Low-speed (5–15 mm/s) to avoid melt impact.
- Medium-speed (20–50 mm/s) for even flow.
- High-speed packing (60–80 mm/s) to compensate shrinkage.
- Packing Pressure: 60–80% of maximum injection pressure.
- Packing Time: 1–1.5 seconds per 1 mm wall thickness.
- Mold Temperature: Match to resin—e.g., 80–120°C for PC, 50–70°C for ABS.
- Screw Speed: Adjust based on melt characteristics, typically 50–150 rpm.
Quality Inspection: Lifecycle Precision Management
- Dimensional Accuracy: Use coordinate measuring machines (CMM) with precision of 0.001 mm. Key dimensions must meet CPK ≥1.33.
- Surface Inspection: Optical microscopy (200×) should reveal no defects ≥0.1 mm (sink marks, flash, etc.).
- Process Traceability: Record pressure, temperature, and cycle data for at least three years.
- Maintenance: After every 500 cycles, inspect parting surfaces, ejector pins, and calibrate measurement equipment regularly.

Process Environment Control: Ensuring Stability
- Ambient Conditions: Maintain workshop at 22±1°C and 50%±5% RH.
- Cleanliness: Class 8 cleanroom standard to prevent dust contamination.
- Vibration Control: Floor vibration amplitude ≤0.01 mm.
- Airflow: Maintain velocity between 0.2–0.5 m/s to avoid mold temperature fluctuations.
Equipment Maintenance: Guaranteeing Long-Term Accuracy
- Hydraulic System: Monthly checks, pressure stability within ±0.5 MPa.
- Screw & Barrel: Inspect quarterly; replace when wear >0.02 mm.
- Temperature Control: Calibrate thermocouples every six months (error ≤±1°C).
- Lubrication: Weekly checks to reduce component wear.
Application of New Technologies
Driving Efficiency and Intelligence
- Smart Sensors: Install in critical areas to monitor temperature, pressure, and displacement in real time, enabling automatic parameter adjustments.
- AI & Machine Learning: Analyze historical production data to predict quality issues and optimize processes proactively.
Conclusion
The essence of precision injection molding lies in micron-level detail control. With standardized process management, product dimensional tolerances can be stabilized within ±0.01 mm, and weight repeatability can reach 0.1%. This ensures robust technical support for high-end manufacturing. Looking forward, the industry is moving toward higher efficiency, greater precision, and intelligent automation, securing precision injection molding’s position as a cornerstone of advanced production.