

Plastic Shrinkage Rate — More Than Just a Number
In plastic injection moulding, the shrinkage rate is not simply a single figure; it is a key system parameter that requires a thorough understanding.
Mould makers rely on it to adjust cavity dimensions, while engineers use it to ensure the dimensional accuracy of moulded components. To fully grasp its importance, we must first examine the fundamental nature of shrinkage in thermoplastics.
What is Shrinkage? Two Core Concepts
During the injection moulding of thermoplastics, part dimensions change as the material cools. These dimensional variations are often referred to as shrinkage or warpage, yet they are not the same:

- Shrinkage: A uniform reduction in overall volume, where the part becomes smaller in size.
- Warpage: A distortion in shape while the overall volume remains unchanged.
For mould designers, accurately predicting the dimensional difference between the cavity and the final part caused by shrinkage is essential. However, this is a complex task, as shrinkage is influenced by multiple factors, including processing temperature, moulding pressure, material behaviour, and part geometry.
Shrinkage is More Than Thermal Contraction
It is a common misconception that shrinkage is purely thermal contraction. In reality, several additional mechanisms play a role:
- Residual stresses
Uneven cooling and temperature gradients within the cavity introduce internal stresses, restricting free shrinkage. - Crystallisation of semi-crystalline plastics
Materials such as PA (Nylon) and PBT form crystalline structures during cooling. The level of crystallisation, and therefore shrinkage, depends on cavity temperature and cooling rate. - Mechanical restraint
Mould constraints and part geometry limit shrinkage. For example, when the outer layer solidifies first, it restricts the inner material from contracting freely.
Furthermore, injection parameters such as holding pressure, gate design, and melt temperature all directly influence shrinkage behaviour.

The p-v-T Relationship: Pressure, Volume, Temperature
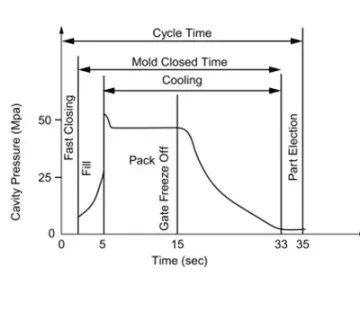
The p-v-T diagram (Pressure–Volume–Temperature) illustrates how thermoplastics change in volume under different process conditions:
- Compressibility: Volume decreases under higher pressures.
- Thermal behaviour: Volume decreases as temperature falls.
From this, both volumetric shrinkage (Sv) and linear shrinkage (Sl) can be derived. These values are fundamental in mould design and dimensional prediction.
Shrinkage is Directional
Shrinkage is not uniform across all dimensions; it is anisotropic and varies by orientation:
- Thickness direction: Shrinkage is most significant, accounting for 90–95% of volumetric shrinkage.
- Length and width directions: Shrinkage is restrained by mould geometry, typically representing only 5–10% of volumetric shrinkage.
This anisotropy often results in warpage or dimensional deviations in the final product.
Shrinkage Over Time: The Hidden Factor
Shrinkage does not end upon demoulding; it continues to evolve over time. The timing of measurement therefore matters:
- Demoulding shrinkage: Immediate dimensional change observed after ejection.
- Moulding shrinkage: Standard industry reference, typically measured 24 hours after moulding under controlled conditions.
- Post-shrinkage: Long-term shrinkage caused by stress relaxation or further crystallisation, often accelerated by heat exposure.
Additionally, certain polymers such as Nylon absorb moisture, leading to further dimensional changes after moulding.

| Column | Description | Index | Measurement Explanation |
|---|---|---|---|
| A | Cold mould dimension | 1 | Initial cold mould measurement |
| B | Hot mould dimension under set pressure | 2 | Dimensional increase due to mould thermal expansion |
| C | Injection-moulded part dimension | 3 | Shrinkage immediately after injection moulding |
| D | Part dimension after 24 hours | 4 | Shrinkage after 24 hours of cooling |
| E | Part dimension after long-term storage | 5–6 | Post-shrinkage / Total material shrinkage |
| F | Part dimension after conditioning (e.g., moisture absorption) | 7 | Dimensional change due to conditioning |
Conclusion: Mastering Shrinkage in Thermoplastics
Shrinkage in thermoplastics is essentially a volumetric change influenced by material properties, process conditions, and part design.
By understanding p-v-T behaviour, the relationship between linear and volumetric shrinkage, and the time-dependent nature of dimensional change, mould makers and engineers can significantly improve prediction accuracy and minimise dimensional errors in injection moulded parts.